
Aluminum Welding on Countersinks? Non-Sticking Solutions
Expert analysis of Aluminum welding on countersinks causes with Lihao Technology exclusive solutions
🔍 Cause Analysis of Aluminum welding on countersinks
1. High Aluminum Adhesion
Aluminum is ductile and welds onto the cutting edge, forming a built-up edge
2. High-Friction Coating
Standard coatings have high friction - chips stick to the tool surface and clog
3. Improper Cutting Parameters
Low speed or feed raises cutting temperature, increasing welding
✅ Lihao Technology Solutions
TiAlN Composite Coating
0.15 friction coefficient - smooth, non-sticking, ideal for aluminum
Mirror-Polished Edges
Ra0.4 mirror polish - chips slide off, less built-up edge
Large Rake Angle Design
15-degree rake cuts sharp and cool, reducing welding
High-Speed Cutting
Recommended 3000-5000rpm - cool high-speed cutting evacuates chips fast, no welding
Recommended Products
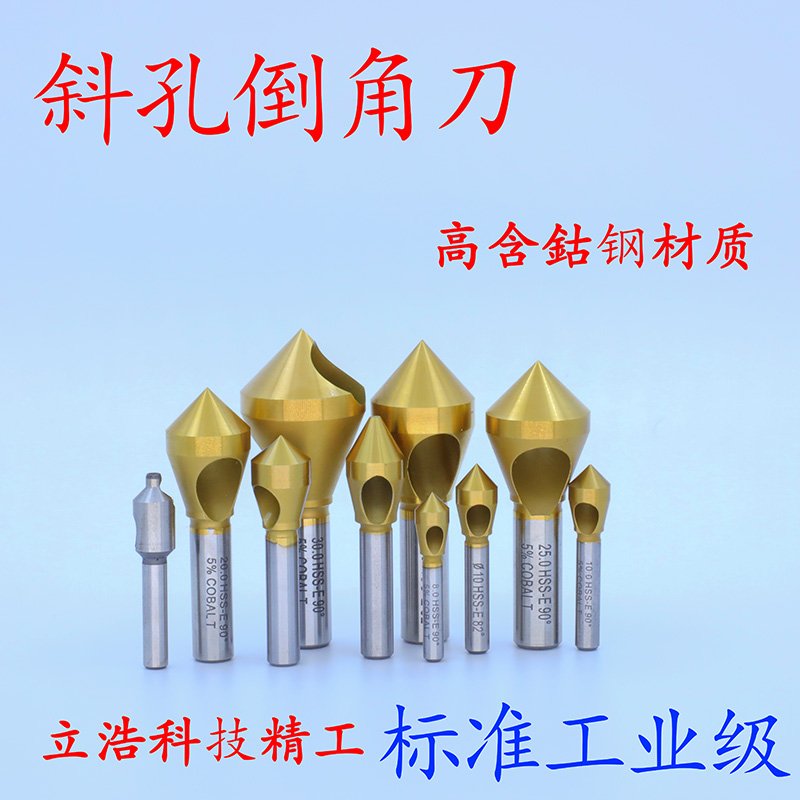
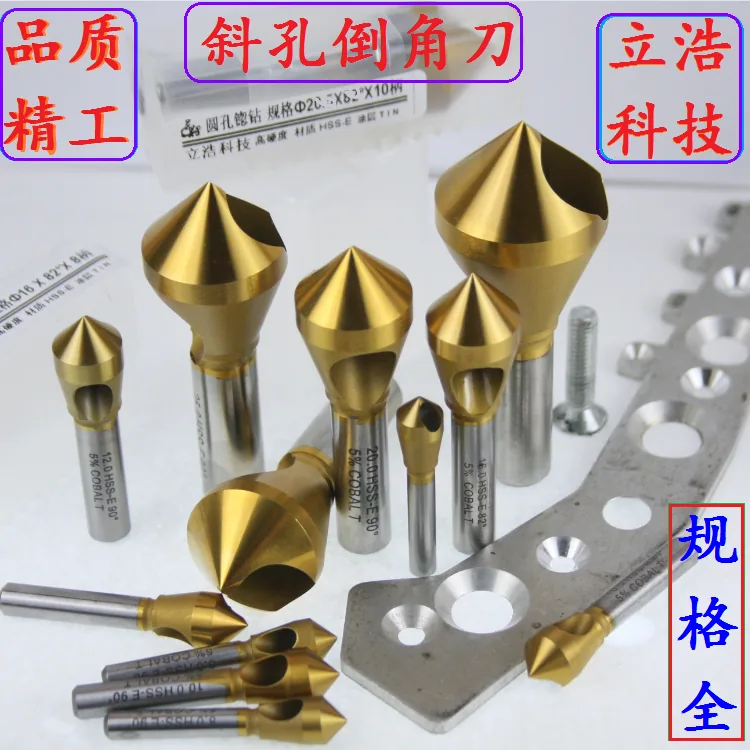
📊 Recommended Cutting Parameters
| Recommended coating | TiAlN composite, 0.15 friction coefficient |
| Edge treatment | Mirror polish Ra0.4 |
| Rake angle | Large 15-degree rake |
| Speed and feed | Adjust per material/machine/tool size; start slow, then increase |
🏆 Customer Cases
Severe chip welding on aluminum - cleaning every 500 parts, rough surface
Lihao TiAlN-coated countersinks - no welding, 1500 parts without cleaning, glossy surface
Facing Aluminum welding on countersinks problems?
Lihao Technology engineers provide one-on-one technical guidance, 48-hour response, 7-day custom manufacturing delivery
WeChat Consultation
WeChat ID: 15338372359
Phone: 15338372359(same as WeChat)