
Burrs on Chamfers? Causes and Solutions
Expert analysis of Burrs on chamfers causes with Lihao Technology exclusive solutions
🔍 Cause Analysis of Burrs on chamfers
1. Insufficient Tool Hardness
Standard HSS below HRC62 wears fast on hard materials like stainless steel, creating burrs
2. Dull Cutting Edges
Poor grinding leaves micro-nicks that tear material and create burrs
3. Improper Cutting Parameters
Speed too low or feed too fast makes cutting unstable and forms burrs
4. Poor Tool Coating
High-friction coatings clog chip flow; chips scrape the hole edge and cause burrs
5. Inaccurate Tool Angle
Loose angle tolerance causes uneven cutting and burrs
✅ Lihao Technology Solutions
Cobalt HSS HRC67
5 degrees harder than standard HSS, tough edges stay sharp cutting stainless steel
Swiss Precision Grinding
ANCA-ground with mirror-polished edges, no micro-nicks, smooth burr-free cutting
TiAlN Composite Coating
0.15 friction coefficient - smooth chip flow, no scraping, glossy chamfers
+/-0.1 Degree Tolerance
Precise angle control for even cutting and smooth burr-free holes
Recommended Products
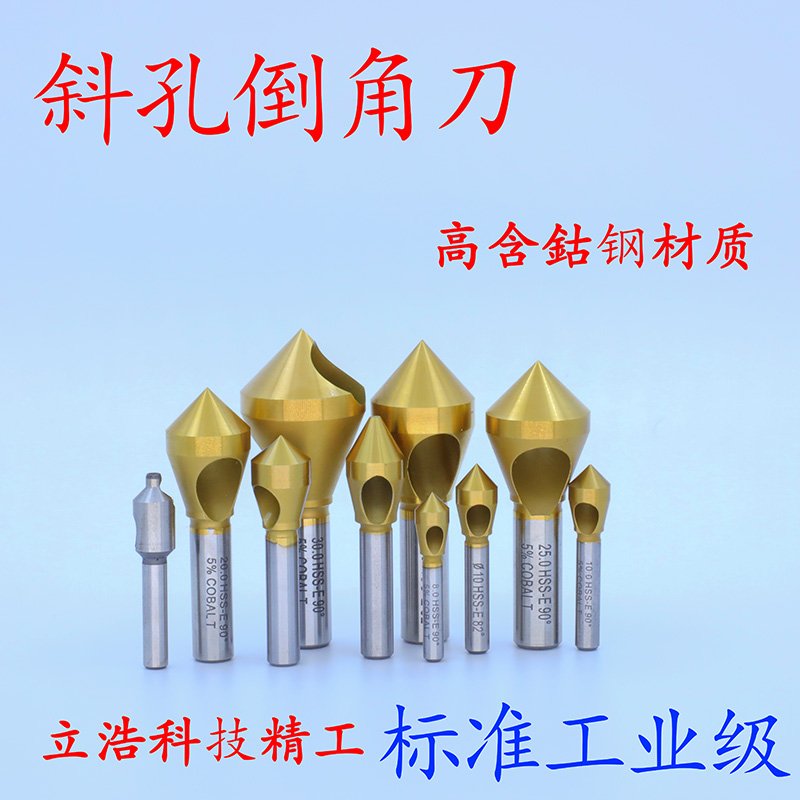
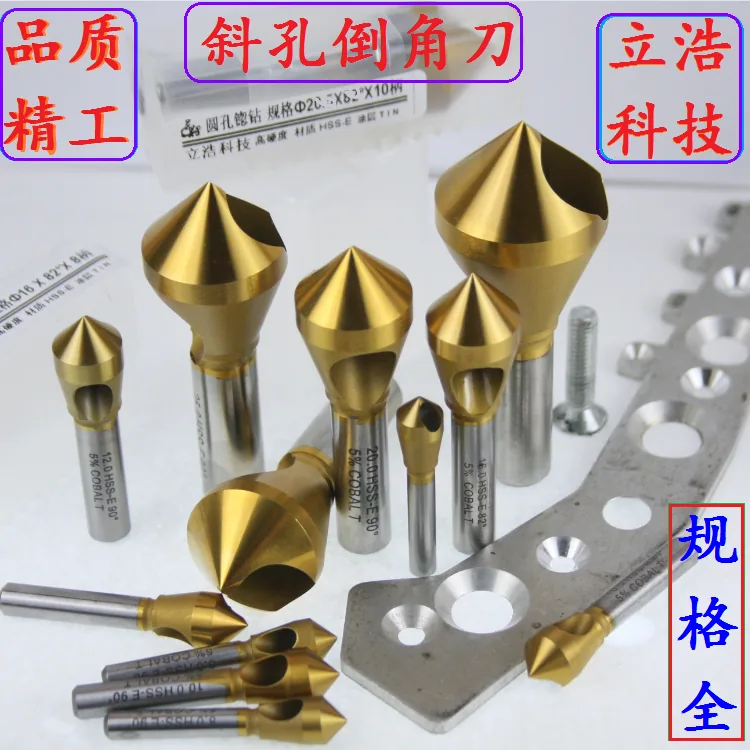
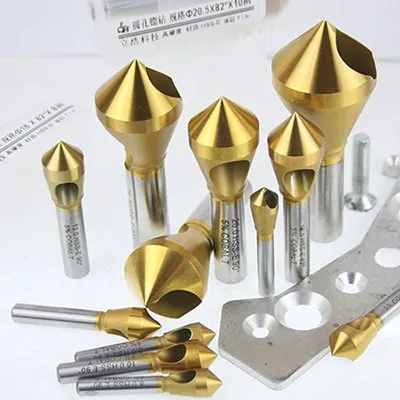
📊 Recommended Cutting Parameters
| Recommended material | Cobalt HSS HRC67 |
| Recommended coating | TiAlN composite coating |
| Speed and feed | Adjust per material/machine/tool size; start slow, then increase |
🏆 Customer Cases
Standard tools left heavy burrs - 30 seconds manual deburring per part, high labor cost, low efficiency
Lihao cobalt HSS countersinks - smooth burr-free chamfers, no manual deburring
Facing Burrs on chamfers problems?
Lihao Technology engineers provide one-on-one technical guidance, 48-hour response, 7-day custom manufacturing delivery
WeChat Consultation
WeChat ID: 15338372359
Phone: 15338372359(same as WeChat)