
Poor Chip Evacuation? Causes and Solutions
Expert analysis of Poor chip evacuation causes with Lihao Technology exclusive solutions
🔍 Cause Analysis of Poor chip evacuation
1. High-Friction Coating
Standard coatings let chips stick to the tool surface, clogging flow
2. Chip Flutes Too Small
Small flutes cannot clear chips, which pile up in the hole
3. Improper Cutting Parameters
Excess feed or low speed makes chips too thick and long to clear
4. Dull Cutting Edges
Dull edges tear material into irregular chips that are hard to clear
✅ Lihao Technology Solutions
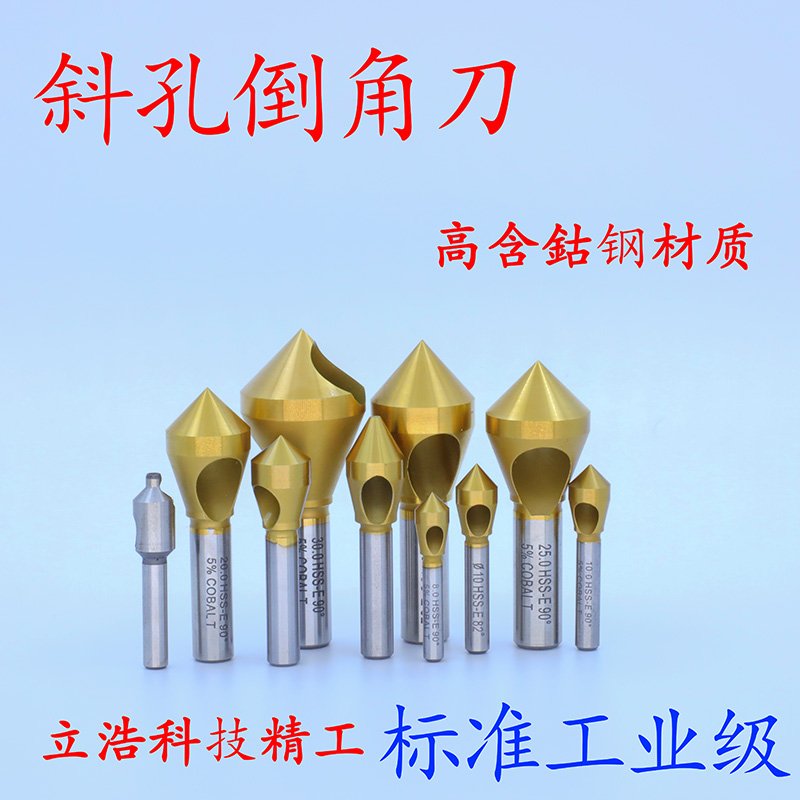
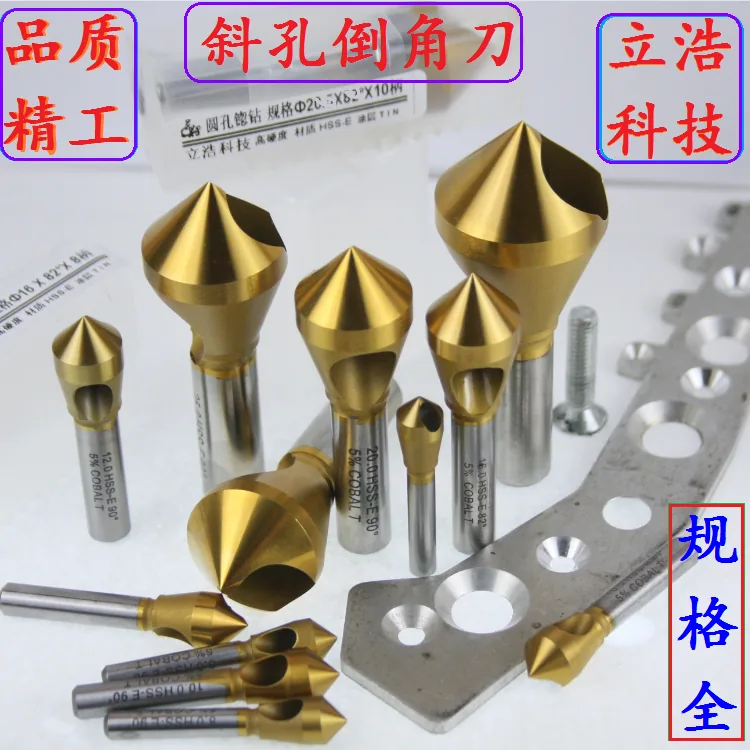
TiAlN Coating, 0.15 Friction
Smooth TiAlN surface - chips do not stick, flow clears easily
Large Chip Flute Design
Optimized large flutes give chips room to clear without piling up
Smooth Cutting with Sharp Edges
Mirror-polished edges cut smoothly, producing regular chips that evacuate easily
Optimized Cutting Parameters
Best parameters per material prevent chips from being too thick or long
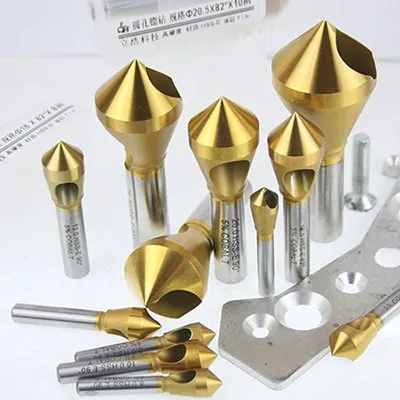
Recommended Products
📊 Recommended Cutting Parameters
| Recommended coating | TiAlN composite, 0.15 friction coefficient |
| Chip flutes | Large flute design |
| Speed | 2000-4000rpm |
| Feed | 0.1-0.2mm/r |
🏆 Customer Cases
Standard tools clogged on aluminum - cleaning each part, 8% defect rate
Lihao TiAlN-coated countersinks - smooth flow, no cleaning, defect rate 1%
Facing Poor chip evacuation problems?
Lihao Technology engineers provide one-on-one technical guidance, 48-hour response, 7-day custom manufacturing delivery
WeChat Consultation
WeChat ID: 15338372359
Phone: 15338372359(same as WeChat)