
Low Chamfering Efficiency? Causes and Solutions
Expert analysis of Low chamfering efficiency causes with Lihao Technology exclusive solutions
🔍 Cause Analysis of Low chamfering efficiency
1. Dull Cutting Edges
Standard dull edges force low speed and feed
2. Too Few Flutes
Single or double-flute tools remove little material per revolution
3. Poor Chip Evacuation
Clogged chips force lower feed, hurting efficiency
4. Frequent Tool Changes
Short tool life means constant changes and setup, wasting time
✅ Lihao Technology Solutions
Sharp Edge Design
Large rake angle and mirror-polished edges - low cutting resistance, allowing high speed and feed
High-Efficiency Cutting Design
Optimized cutting angles remove more material per revolution - 40% higher efficiency
Smooth Chip Flow with TiAlN
0.15 friction coefficient - high feed without clogging
Long Life, Fewer Changes
Cobalt HSS + TiAlN - 3x life, less changeover time
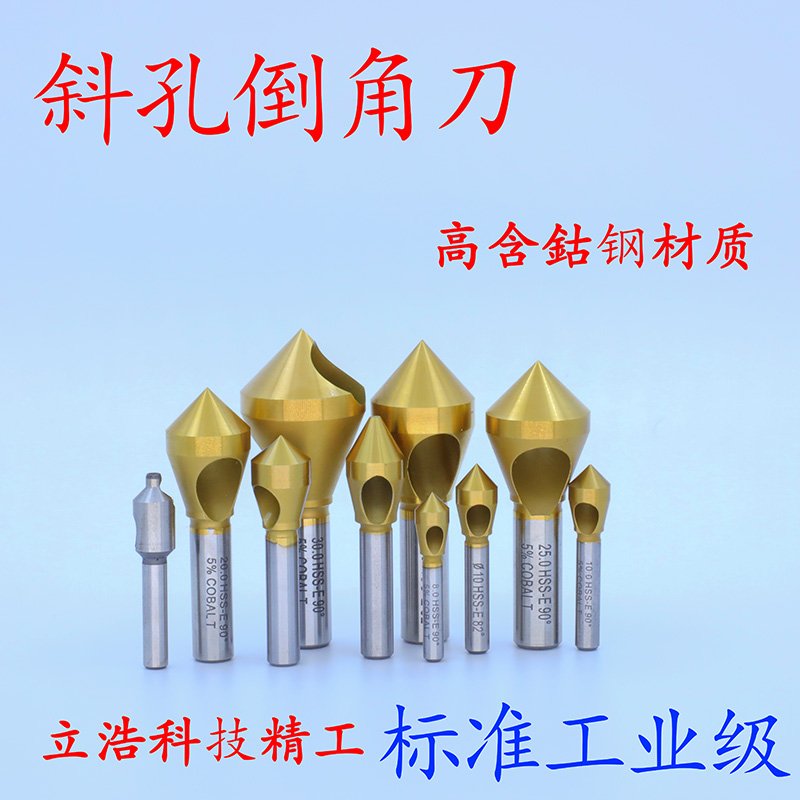
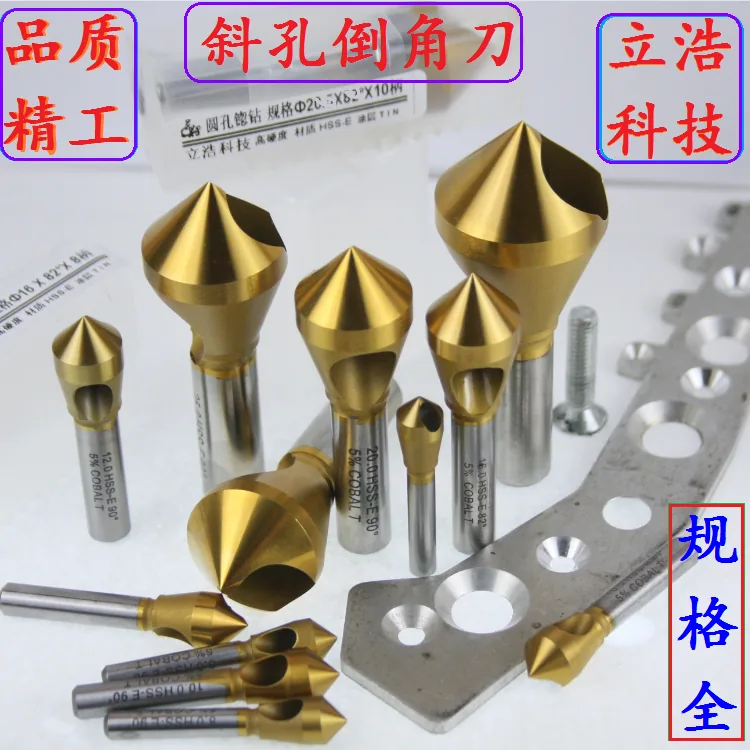
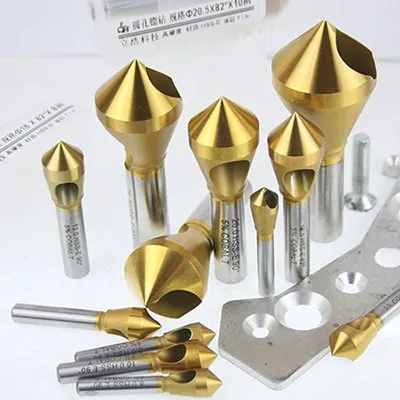
Recommended Products
📊 Recommended Cutting Parameters
| Cutting design | Optimized high-efficiency angles |
| Efficiency gain | 40% higher than standard tools |
| Speed and feed | Adjust per material/machine/tool size; start slow, then increase |
🏆 Customer Cases
Standard tools - 3 seconds chamfering per part, 8,000 parts per day
Lihao high-efficiency countersinks - 1.8 seconds per part, 13,000 parts per day
Facing Low chamfering efficiency problems?
Lihao Technology engineers provide one-on-one technical guidance, 48-hour response, 7-day custom manufacturing delivery
WeChat Consultation
WeChat ID: 15338372359
Phone: 15338372359(same as WeChat)