
Countersink Vibration Marks? Causes and Solutions
Expert analysis of Countersink vibration marks causes with Lihao Technology exclusive solutions
🔍 Cause Analysis of Countersink vibration marks
1. Insufficient Tool Rigidity
Shank too thin or long - vibration during cutting leaves marks
2. Poor Dynamic Balance
Asymmetric flutes vibrate at high speed, marking the surface
3. Insufficient Machine Rigidity
Weak spindle or fixture causes resonance during cutting
4. Improper Cutting Parameters
Speed or feed too high makes cutting force fluctuate, causing marks
✅ Lihao Technology Solutions
Thicker Shank Design
20% thicker shank, 40% higher rigidity - stable cutting, no vibration marks
Precision Dynamic Balancing
G2.5 balancing on every tool before shipping - no vibration at high speed
Symmetric Multi-Flute Design
3/6-flute symmetric design spreads cutting force evenly, reducing vibration
Optimized Cutting Parameters
Best parameters per material and machine to avoid resonance zones
Recommended Products
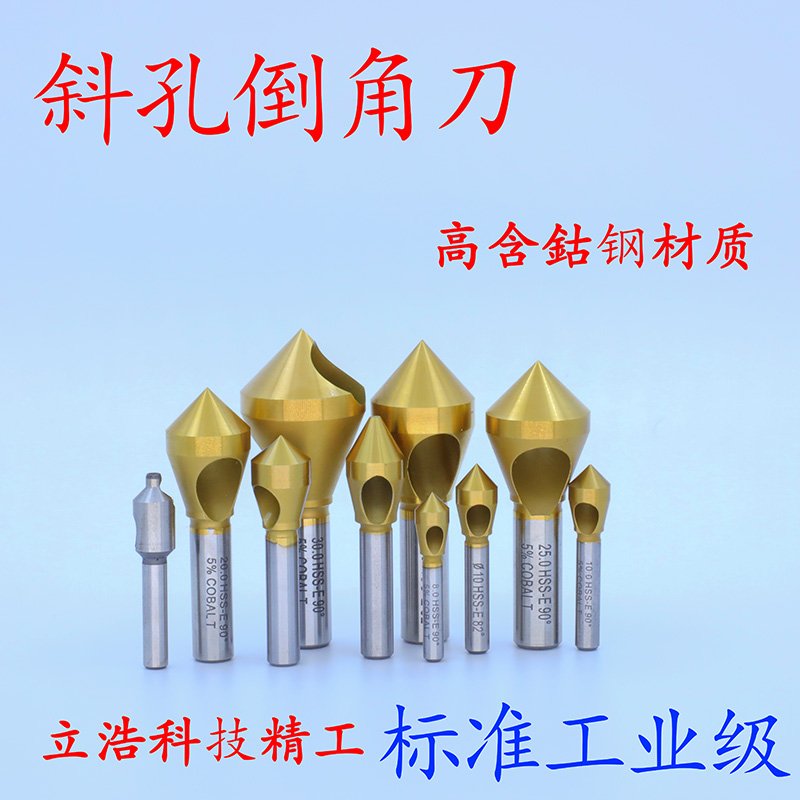
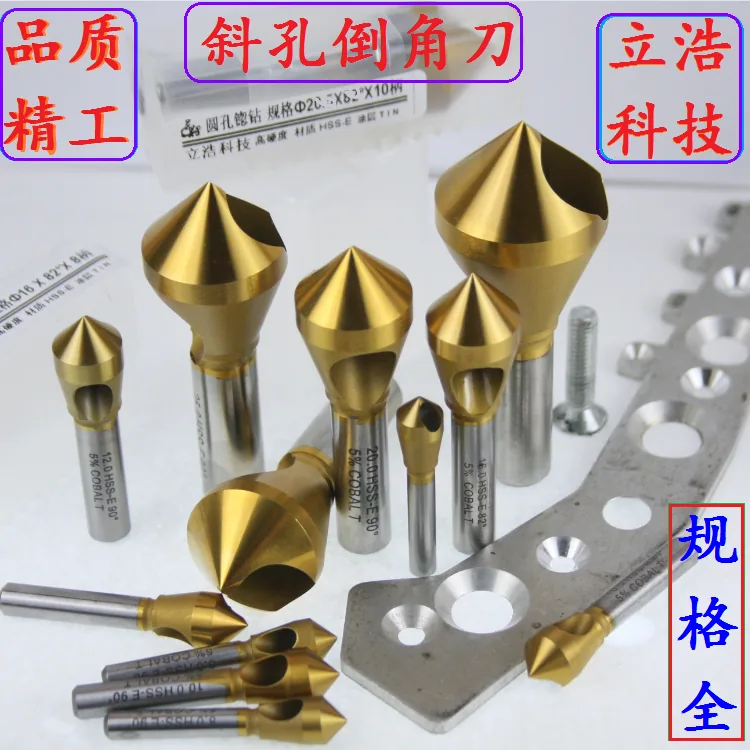
📊 Recommended Cutting Parameters
| Recommended shank | Thick shank, 40% higher rigidity |
| Balancing grade | G2.5 |
| Flutes | 3/6-flute symmetric |
| Speed and feed | Adjust per material/machine/tool size; start slow, then increase |
🏆 Customer Cases
Standard tools showed obvious vibration marks, surface roughness Ra3.2, below automotive requirements
Lihao thick-shank high-rigidity countersinks - smooth, no marks, Ra0.8
Facing Countersink vibration marks problems?
Lihao Technology engineers provide one-on-one technical guidance, 48-hour response, 7-day custom manufacturing delivery
WeChat Consultation
WeChat ID: 15338372359
Phone: 15338372359(same as WeChat)